A backpack that changes color with temperature, a laptop bag with an advanced moisture barrier, or a travel bag made with a coating capable of repairing minor scratches might sound futuristic. Yet textile research is already exploring the materials needed to make these ideas possible.
Functional textiles are changing how designers approach everyday accessories. Instead of selecting fabrics primarily for appearance, weight, and cost, manufacturers can now explore materials engineered to respond to environmental conditions, improve structural performance, and address specific product challenges.
For the bag manufacturing industry, this creates opportunities to develop products with more specialized features. However, not every emerging textile technology is ready for large-scale commercial production.
Some materials, such as three-dimensional spacer fabrics, already have established applications. Others, including self-healing coatings, remain areas of active research and development.
Four technologies deserve particular attention: 3D spacer fabrics, thermochromic textiles, electrospun nanofiber membranes, and self-healing textile coatings.
Understanding their properties, manufacturing requirements, and limitations can help textile professionals and product developers make better material decisions.
Table of Contents
1. 3D Spacer Fabrics: Improving Comfort Through Textile Structure
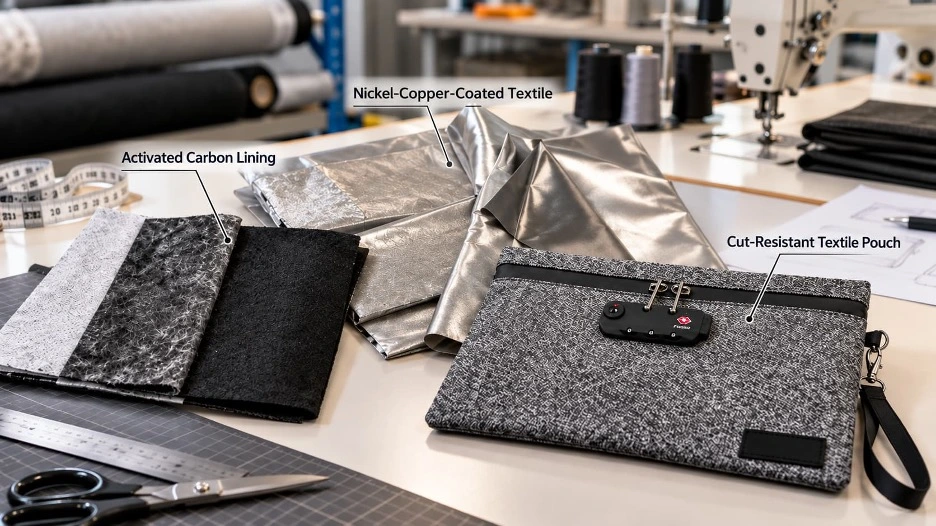
Traditional backpack padding often combines foam with an outer textile layer. Although this construction provides cushioning, it can also create challenges involving ventilation, flexibility, and moisture accumulation.
Three-dimensional spacer fabrics offer an alternative approach by building cushioning and air spaces directly into the textile structure.
How 3D Spacer Fabrics Work
A 3D spacer fabric consists of two separate textile surfaces connected by yarns that maintain a defined distance between them.
These connecting yarns, often made from synthetic monofilaments, create an internal structure that can provide resilience and compression recovery.
Spacer fabrics are commonly produced using specialized knitting technology, including double-needle-bar warp knitting machines.
Their physical characteristics depend on several construction variables:
- Yarn type and filament diameter.
- Distance between the outer fabric surfaces.
- Knitting density and stitch configuration.
- Arrangement and inclination of connecting yarns.
- Thickness and flexibility of the finished structure.
Applications in Modern Backpacks
One practical application is the back panel of a commuter or hiking backpack. When a conventional padded panel rests directly against the wearer’s back, heat and perspiration can accumulate during extended use.
A suitably designed spacer fabric can introduce air channels while providing cushioning between the bag and the body. These structures may also be incorporated into shoulder straps, laptop sleeves, and protective equipment compartments.
For manufacturers, the main benefit is design flexibility. Rather than using the same padding arrangement throughout a bag, different spacer constructions can be selected according to the pressure and ventilation requirements of each area.
Manufacturing Challenges
Spacer fabrics require careful consideration during cutting and assembly. Compression under stitching, seam placement, and the interaction between spacer layers and surrounding materials can affect their performance.
A fabric demonstrating excellent compression recovery in laboratory testing may behave differently when tightly enclosed inside a finished backpack panel. Manufacturers should therefore evaluate thickness retention, repeated compression, air permeability, and comfort during actual product use.
2. Thermochromic Textiles: Creating Bags That Respond to Temperature
Imagine a travel accessory that changes its appearance when exposed to warmth or a backpack featuring a decorative panel that reacts to temperature variations. Thermochromic textiles make these visual effects possible.
Unlike conventional dyed materials, thermochromic fabrics contain substances whose optical properties change within particular temperature ranges.
The Science Behind Color-Changing Textiles
Many thermochromic textile systems use temperature-sensitive pigments or microencapsulated color-changing compounds.
Depending on the formulation, these materials may become lighter, darker, transparent, or change between different colors when their temperature crosses a specified threshold.
Reversible thermochromic systems can return toward their original appearance when the temperature changes back.
Microencapsulation is particularly important because it can help protect sensitive color-changing components and support their incorporation into coatings or printing formulations. For textile applications, these materials may be applied using techniques such as screen printing or specialized finishing processes.
However, temperature sensitivity varies considerably between formulations. A pigment designed to change color near normal room temperature will behave differently from one developed for much warmer conditions.
Potential Applications in Bag Design
Thermochromic materials could introduce new design possibilities for:
- Fashion backpacks with temperature-responsive graphics.
- Children’s school bags featuring interactive visual elements.
- Travel accessories with changing decorative patterns.
- Promotional bags using temperature-sensitive printed designs.
Consider a backpack featuring a thermochromic graphic on its front panel.
The printed design might change when touched by a warm hand or exposed to sunlight. Such an effect could create an interactive aesthetic without requiring batteries or electronic components.
The technology may also have potential for visual temperature indication, although an accurate temperature-monitoring application would require appropriate calibration and testing.
A decorative color change should never automatically be interpreted as a reliable measurement of temperature.
Durability and Production Considerations
The main challenge is maintaining consistent color-changing performance throughout the product’s expected lifespan. Thermochromic pigments may be sensitive to ultraviolet exposure, repeated heating, abrasion, and cleaning.
The surrounding binder, coating thickness, substrate, and application process can also influence the final appearance.
For manufacturers, suitable evaluation procedures may include repeated thermal cycling, color measurements, rubbing tests, and exposure to expected environmental conditions.
Material compatibility deserves particular attention when thermochromic printing is applied to coated nylon or polyester.
Excessive processing temperatures or unsuitable chemicals may affect the functional pigments. Brands should also consider whether the visual effect provides sufficient practical or aesthetic value to justify the additional production cost.
3. Electrospun Nanofiber Membranes: Exploring Advanced Moisture Protection
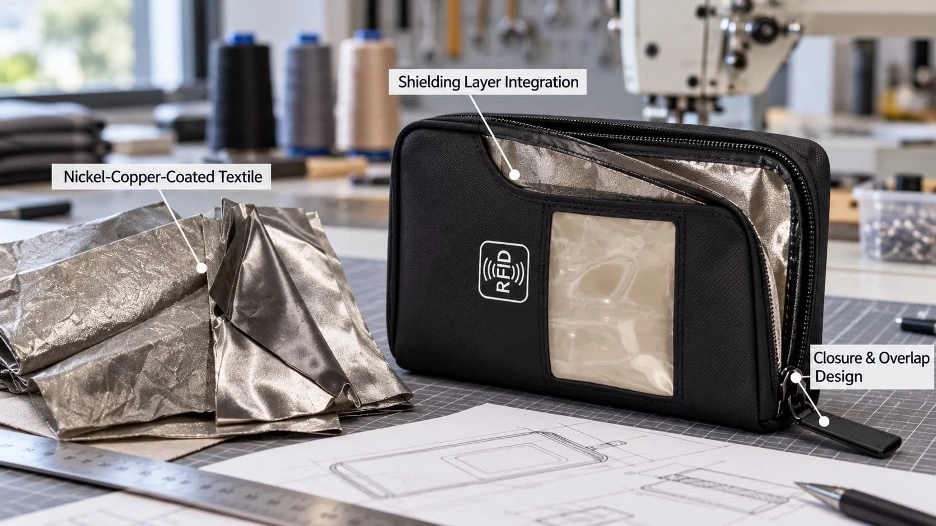
Outdoor backpacks and equipment bags often need to protect their contents from rain while remaining reasonably lightweight and flexible.
Conventional waterproofing approaches include polymer coatings, laminated membranes, and water-repellent fabric finishes. Electrospun nanofiber membranes represent another area of development in protective textiles.
Understanding Electrospinning Technology
Electrospinning uses an electric field to draw extremely fine fibers from a suitable polymer solution or melt. The resulting fibers can form a nonwoven membrane containing a network of interconnected pores.
Depending on the polymer chemistry, fiber dimensions, pore structure, and surface treatment, these membranes can be engineered to resist liquid water while allowing moisture vapor to pass through.
Waterproofness concerns resistance to liquid water penetration, while moisture-vapor permeability describes how readily water vapor moves through a material.
A textile can perform well in one area without necessarily delivering the same level of performance in the other.
Researchers are investigating electrospun membranes made from various polymer systems, including polyurethane-based materials, for protective textile applications.
Opportunities for Technical Bag Manufacturing
Electrospun membranes could be incorporated into laminated textile structures intended for:
- Outdoor equipment bags exposed to changing weather.
- Technical backpacks requiring lightweight moisture barriers.
- Protective storage compartments.
- Specialized carrying accessories where vapor transport is beneficial.
From Textile Development to Commercial Production
One challenge with electrospun membranes is that extremely fine fiber structures may require additional support to withstand abrasion, handling, and repeated flexing.
Laminating a membrane to a woven or knitted backing can improve usability, but the bonding process must be carefully controlled. Excessive adhesive application may restrict vapor transmission, while insufficient bonding can lead to delamination.
For a brand working with a bag manufacturer, early prototype development can help determine whether an advanced membrane is necessary or whether a conventional coated fabric already provides adequate protection.
Testing should consider hydrostatic pressure resistance, moisture-vapor transmission, flex durability, seam construction, and the finished bag’s resistance to water entry.
A technically impressive laminate is of limited value if rainwater enters through unprotected stitching or zipper openings.
4. Self-Healing Textile Coatings: A New Direction in Material Durability
Scratches, surface cracks, and coating damage can gradually affect the appearance and performance of bags. For products using polymer-coated fabrics, repeated folding, friction, and environmental exposure may eventually contribute to visible wear.
Researchers are investigating self-healing polymer coatings as one possible way to address certain forms of minor material damage.
How Self-Healing Coatings Function
Self-healing materials are designed to recover selected properties after damage under suitable conditions. Some systems contain microcapsules that release a repair substance when damaged. Others rely on reversible molecular interactions that allow parts of the polymer network to reorganize.
Certain polyurethane-based coatings use dynamic chemical bonds that can reform when exposed to an appropriate stimulus, such as heat.
For example, experimental systems incorporating reversible bonds have demonstrated the ability to repair small coating defects under controlled laboratory conditions.
However, these findings should not be interpreted as evidence that a finished bag can repair every scratch or tear during ordinary use. Healing efficiency depends on the polymer formulation, extent of damage, treatment conditions, and number of repair cycles.
Potential Uses in Bag Manufacturing
If developed into commercially practical textile systems, self-healing coatings could offer possibilities for:
- Premium travel bags with coated exterior surfaces.
- Protective equipment cases.
- Technical backpacks exposed to frequent handling.
- Reusable accessories designed for extended service life.
Consider a coated travel bag that develops small surface scratches during regular transportation.
A suitable self-healing coating might recover some of its surface integrity under specified conditions, potentially helping preserve appearance or selected functional properties.
Self-healing should therefore be understood as a material-specific capability rather than a general guarantee of product durability.
Commercial and Technical Limitations
Self-healing coatings remain an emerging technology, particularly for broad consumer bag applications. Several challenges must be resolved before wider adoption becomes practical.
These include coating flexibility, production costs, long-term performance, resistance to repeated damage, and compatibility with existing textile finishing processes.
Manufacturers must also consider whether the healing mechanism requires elevated temperatures or other conditions unsuitable for everyday users. A coating that performs well under controlled laboratory conditions may offer limited practical value if its repair process is difficult to reproduce safely.
Environmental considerations matter as well. Adding complex polymer layers may affect the recyclability of textile products. Any durability or sustainability claims should therefore be supported by appropriate evidence, including realistic product-use testing.
What These Four Technologies Mean for Future Bag Development
The four textile technologies address different design requirements, making them more useful for some products than others.
| Functional textile | Primary function | Potential bag application |
| 3D spacer fabrics | Cushioning, airflow, and compression recovery | Backpack panels and shoulder straps |
| Thermochromic textiles | Temperature-responsive color changes | Interactive fashion bags and accessories |
| Electrospun nanofiber membranes | Engineered moisture-barrier performance | Technical outdoor bags and protective panels |
| Self-healing coatings | Recovery from certain forms of minor coating damage | Coated travel bags and protective cases |
The most important consideration is whether the selected material improves the finished product in a meaningful way.
A commuter backpack may benefit more from a well-engineered spacer panel than from an expensive experimental coating. Similarly, a fashion accessory may use thermochromic printing successfully without requiring changes to its entire structural construction.
Material selection should begin with the intended application, followed by performance requirements, cost analysis, prototype development, and manufacturing feasibility.
Why Product-Level Testing Still Matters
Functional textile performance is usually established under defined testing conditions. However, manufacturing introduces variables that may change how a material behaves.
Sewing, cutting, lamination, adhesive bonding, folding, and repeated handling can all affect the finished structure.
A practical development process should include:
- Defining the required performance and intended use.
- Reviewing material specifications and relevant technical research.
- Selecting appropriate testing methods.
- Producing representative prototypes.
- Evaluating the finished product under realistic conditions.
- Confirming repeatability before large-scale production.
Functional textiles are transforming bag manufacturing by introducing new possibilities for comfort, durability, protection, and interactive design. From breathable 3D spacer fabrics and color-changing thermochromic materials to electrospun nanofiber membranes and self-healing coatings, these technologies offer innovative ways to improve everyday accessories.
However, successful innovation depends on selecting materials that solve practical problems rather than simply adding advanced features. By combining thoughtful textile selection, reliable testing, and efficient manufacturing methods, brands can develop functional bags that balance performance, durability, and user expectations.

Mahedi Hasan working as an Executive (Fabric Marketing) at Pengnuo Group. Graduated with B.Sc. in Textile Engineering. Before was a Top Rated content writer at Upwork, and Level 02 Seller at Fiverr, Level 02 Publisher at Ezoic. Very passionate about content writing, SEO practice, and fashion website designing. Highly Experienced fashion writer for the last 4+ years. Have extensive 7 years of experience in the wholesale clothing business.